Belt Conveyors Systems Manufacturer
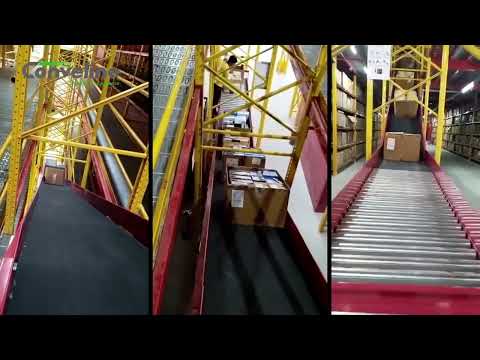
Conveline offers a wide range of advanced belt conveyor systems designed to enhance efficiency in intralogistics operations. As a trusted Belt Conveyors Systems Manufacturer, Conveline provides versatile models, including horizontal and power feeder configurations, tailored to meet diverse operational needs. These belt conveyors are equipped with intermediate and direct drive options, ensuring reliable and seamless performance across various applications. The innovative Conveline Belt Conveyor sets new standards with its ability to handle unit loads of up to 50 kg (110 lbs.) at impressive speeds of up to 150 mpm. Designed for durability and efficiency, these conveyors are an ideal solution for businesses seeking optimized material handling systems. With a focus on precision engineering and robust functionality, Conveline ensures that its belt conveyor systems deliver consistent performance, making them a valuable addition to any production or logistics environment.

Specs at a Glance
Request a Quote- Structure
- Aluminium
- Widths
- 450 / 650 / 850 / 1050 mm
- Lengths
- 400–20000 mm
- Total Load
- Up to 50 kg per metre
- Speed
- Up to 150 m/min
- Configurations
- Straight, Incline, Decline and Curved
- Drive Options
- 24V and 400V
- Rated Voltage
- 400V
Features
- Highest throughput possible:
- up to 150 mpm
- Best lead times
- for standard and custom systems plus local planning support by experienced application engineers
- 24V and 400V drive options
- for energy efficiency all the way
- Flexible side guides
- Roller conveline make
- for fast and easy maintenance and top mounting
- Versatile Aluminium side profiles
- for simple and flexible installation and system extensions
- Electromechanical actuators Options for efficient and low-noise operation
- Pneumatics Standard option
- High-speed field bus
- as open platform and future-proof control system
Options
- Motor Mounting positions
- Adjustable support leg
- Fully adjustable Guide and Fixed guide
- Customise conveyor layout
- Automations support
- Diverter, Merger, Stopper, etc application
Application
With over more than 50 variants, you can show your customers how to use their processes accelerate. Conveline intralogistics continues to work on the expansion and optimization of the pre-roofed systems, so that you are always up-to-date with the latest technology. All best practice solutions can be adapted to the individual needs and building conditions on site at your customers. If you have any questions, please contact our conveline intralogistics application support.
- Complex three-dimensional track-layouts without separating points and transitions with one conveyor
- Logistic and warehousing application
- Tote and boxes handling
- Post and parcel application
- End of line automation for carton handling
- product buffer or accumulation application
- Energy saving application
- 400V and 24V option working
Specifications
- Structure available Aluminium
- Widths: 450, 650, 850, 1050 mm
- Lengths: 400-20000 mm
- Total load: typically up to 50 kg per mtr
- Speed: up to 150 m/min
- Options: Straight, incline, Decline and curved
- Rated Voltage: 400V
- *Other values available on request