Roller Conveyor Systems Manufacturer
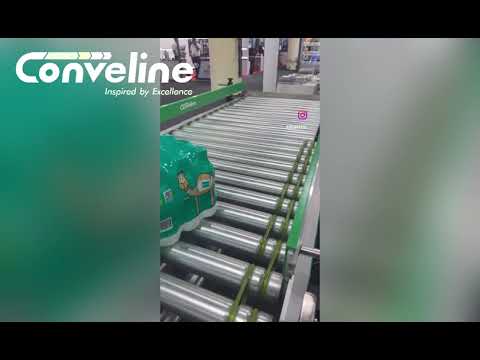
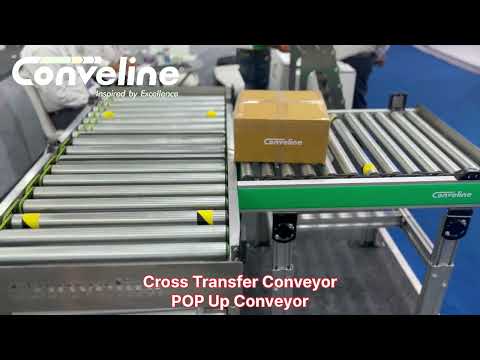
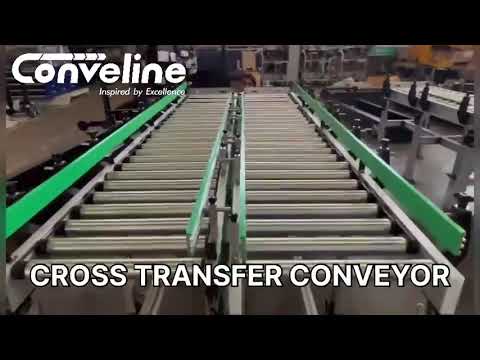
Conveline Systems, a renowned roller conveyor systems manufacturer, specializes in delivering efficient and reliable solutions tailored to enhance workflows across diverse industries. Our advanced roller conveyor systems are designed to streamline material handling, boost productivity, and minimize operational bottlenecks. Whether for manufacturing, warehousing, or distribution, these systems ensure seamless transport of goods with precision and consistency. Engineered for durability and performance, Conveline's roller conveyor systems cater to the unique requirements of each business, offering customization options for length, load capacity, and operational speed. Our commitment to quality and innovation ensures that every system meets the highest industry standards, providing long-term value and dependability. Choose Conveline Systems for cutting-edge conveyor solutions that optimize efficiency and simplify material flow. With our expertise and dedication, we help businesses achieve smoother operations and enhanced productivity through state-of-the-art roller conveyor system

Specs at a Glance
Request a Quote- Standard Width
- 1000–1500 mm
- Standard Length
- 1200–6000 mm
- Frame Thickness
- 5 mm
- Roller Diameter
- 76 mm / 89 mm
- Roller Pitch
- 100 / 150 / 200 mm
- Load Capacity
- 500–1500 kg
- Conveying Speed
- 5–15 m/min
Features
- Maximum length of the standard chain conveyor is 6,000mm.
- Simple construction, stable conveying of product.
- Complies with international safety standards.
- Modular design, easy installation and maintenance.
- Improve warehouse flow and decrease traffic
- Minimize labor load handling.
- Gentle handling - reduce product damage / precision and positioning.
- Improve system throughput, safety, ergonomics.
- Free up fork truck equipment for other tasks.
Options
- Motor Mounting positions
- Support leg
- Fixed guide
- Customise conveyor layout
- Automations support
Application
- Pallet handling application
- Flexible for all distribution channels
- Accumulation can be used as process buffer
- Excellent ability to sort groups of pallet into specific area for procession and shipping
- Can merge and sort pallet by variable areas
- Warehouses and distribution automation
- Integration partners use as AS/RS, picking software's, autonomous mobile robots, palletizer, etc.
- Easy to assemble module application or variable site changes applications
Specifications
- Modern, ergonomic, Heavy duty design
- Standard Width 1000mm to 1500mm
- Standard Length 1200mm to 6000mm
- Frame Thickness 5mm
- Rollers 76mm or 89mm with single or Double sprocket
- Roller Pitch 100mm, 150mm, 200mm
- Load capacity 500kg to 1500kg
- Speed from 5m/min to 15m/min