- Conveline Systems
- 08 Sep 2026
- Blogs
Key Takeaways
- Pallet conveyor systems significantly reduce labor costs by 40-60% through automation.
- Enhanced safety profiles with pallet conveyor systems eliminate risks associated with manual handling.
- Consistent throughput ensures steady flow of pallets, improving overall operational efficiency.
- Space optimization with conveyor systems maximizes storage capacity in tight facilities.
- Conveline Systems Pvt.Ltd. provides custom solutions as a leading pallet conveyor systems manufacturer.
Conveline Systems Pvt.Ltd. is a Leading Manufacturer of Pallet Conveyor Systems.
The Hidden Bottleneck Slowing Your Warehouse Down
Manual pallet handling eats up time, labor, and safety margins faster than most operations realize. Workers strain under heavy loads, forklifts create traffic congestion, and productivity stalls at every transfer point. Meanwhile, competitors who've automated their pallet flow move goods faster, safer, and more consistently. Pallet conveyor systems eliminate these bottlenecks, transforming how facilities handle unit loads from receiving to shipping. The question isn't whether automation makes sense—it's how quickly you can implement it.
Understanding Pallet Conveyor Systems
Pallet conveyor systems are engineered specifically to transport loaded pallets through facilities without manual intervention or forklift dependency. These robust systems handle weights ranging from 500 kg to over 2,000 kg per pallet, moving goods reliably across production floors, warehouses, and distribution centers.
Core components typically include:
- Heavy-Duty Frames: Built to withstand continuous industrial use
- Powered Rollers or Chains: Drive pallets forward with consistent force
- Sensors and Controls: Detect pallet presence and manage flow automatically
- Safety Features: Emergency stops, guards, and overload protection
Pallet Conveyor Systems Manufacturer partners design these elements to work seamlessly together.
Core Benefits Driving Adoption
1. Dramatic Labor Savings
Manual pallet movement requires multiple workers or constant forklift operation. Automated systems handle the heavy lifting, freeing staff for higher-value tasks. Facilities report 40-60% reductions in labor hours dedicated to pallet transport after installation.
2. Enhanced Safety Profiles
Forklift-pedestrian interactions cause numerous warehouse accidents annually. Pallet conveyors separate people from moving loads, dramatically reducing injury risks. No more strained backs, crushed toes, or near-miss incidents at busy intersections.
3. Consistent Throughput
Human operators fatigue. Forklifts need refueling or recharging. Conveyor systems run continuously at predictable speeds, maintaining steady flow regardless of shift changes or breaks. This consistency improves planning accuracy and customer delivery commitments.
4. Space Optimization
Conveyors occupy less floor space than forklift aisles and can utilize vertical space through multi-level configurations. This efficiency becomes crucial in facilities where expansion isn't possible.
5. Reduced Product Damage
Smooth, controlled movement eliminates the jolts and impacts common with manual handling. Fragile goods arrive at destination points in better condition, lowering waste and customer complaints.
Real-World Applications Across Industries
Manufacturing Assembly Lines
Automotive plants move chassis components between workstations. Food processors transport raw materials to processing areas. Pharmaceutical facilities handle ingredient pallets through controlled environments. Conveline Systems Pvt.Ltd. has deployed systems across all these sectors with customized configurations.
Warehouse Receiving and Shipping
Incoming pallets flow directly from dock doors to staging or storage areas. Outbound loads move efficiently to loading bays. Cross-docking operations benefit from rapid transfer capabilities without intermediate storage.
Cold Storage Facilities
Automated systems reduce time doors stay open and minimize worker exposure to extreme temperatures. Specialized components withstand freezing conditions while maintaining reliable operation.
Distribution Centers
High-volume facilities sort pallets by destination, route them to appropriate zones, and stage them for loading—all automatically. This capability becomes essential during peak seasons when manual handling can't keep pace.
Beverage and Bottling Operations
Full pallet loads of beverages move from production to packaging to storage without manual intervention. The weight and volume make automation particularly valuable here.
Types of Pallet Conveyor Configurations
Different applications demand different approaches:
- Chain-Driven Live Roller (CDLR): Chains beneath rollers provide positive drive, ideal for heavy or uneven-bottom pallets. Common in manufacturing and cold storage where reliability matters most.
- Belt-Driven Live Roller (BDLR): Belts offer smoother, quieter operation with easier maintenance. Well-suited for distribution centers and facilities prioritizing noise reduction.
- Pallet Transfer Cars: Move pallets perpendicular to main conveyor lines, enabling complex routing without additional conveyor sections.
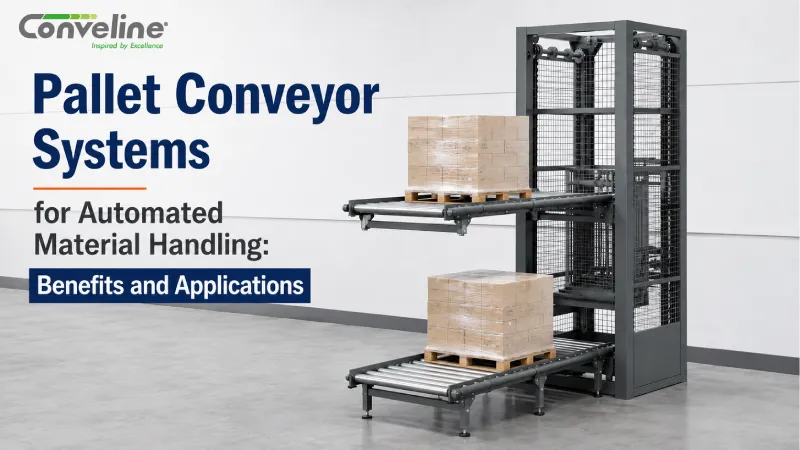
- Vertical Lifts: Raise or lower pallets between floor levels, maximizing cubic space utilization. Pallet Conveyor Systems Manufacturer experts integrate these with horizontal systems for complete automation.
- Accumulation Zones: Allow pallets to queue without backpressure, preventing jams and enabling batch processing.
Integration with Warehouse Management Systems
Modern pallet conveyors don't operate in isolation. They connect with WMS and ERP platforms to:
- Track pallet locations in real-time
- Prioritize movements based on order urgency
- Generate performance metrics for continuous improvement
- Notify operators of maintenance requirements prior to malfunctions.
This connectivity transforms conveyors from simple transport into intelligent material flow management tools.
Key Selection Criteria
Evaluation of the correct conveyor is vital to success:
- Load Capacity: Maximum load capacity, dimensions of pallet, and bottom of load
- Throughput Capacity: Number of pallets per hour
- Floor Plans: Available floor space and ceiling height
- Environment: Temperature, humidity, dust, and washdown considerations
- Scale: Future scale-up and floor plan changes
Expert Pallet Conveyor Systems Manufacturer will help make the decision process easy for you based on their experience.
Maintenance and Longevity Considerations
The quality systems provide years of reliable operation with proper maintenance:
- Lubrication: Keep bearing and drive system parts well lubricated
- Sensor Adjustment: Ensure correct detection and positioning of pallets
- Tension of Belt/Chain: Ensure regular adjustments to avoid any slipping or wear
- Frame Inspection: Inspect frame for any damage, particularly those in areas with high traffic
Maintenance services are offered by Conveline Systems Pvt.Ltd. that prolong system lifetime and help reduce unexpected downtimes.
ROI Beyond Initial Investment
While capital expenditure matters, total value includes:
- Reduced labor costs over system lifetime
- Lower injury-related expenses and insurance premiums
- Decreased product damage and waste
- Improved customer satisfaction from faster, more reliable fulfillment
- Enhanced facility safety ratings and compliance
These factors combine to deliver compelling returns that justify investment decisions.
Why Choose us
Conveline Systems Pvt.Ltd. stands out from the crowd as a reliable Pallet Conveyor Systems Manufacturer owing to our high-quality engineering skills, customizability, and constant customer support services. Not only do we not offer ready-made solutions but also develop systems according to your unique needs and restrictions. We are comprised of experts with many years of industry experience who understand your problems well enough to offer the best configurations for you.
Conclusion
The use of pallet conveyors for automation of material handling provides an already proven way of achieving better efficiency, better safety and better cost control. Companies in the manufacturing, warehousing, and distribution industries have realized that automation is no longer a choice but a necessity. Conveline Systems Pvt.Ltd. has provided many firms with such an experience through provision of systems that are reliable and backed by competent professionals. With labor charges increasing and customers demanding more, the need for automation is becoming even more compelling.Ready to automate your pallet handling operations and unlock significant efficiency gains? Conveline Systems Pvt.Ltd. offers comprehensive consultation and custom-engineered pallet conveyor solutions designed for your unique requirements.
Discover how our systems can transform your material flow and reduce operational costs. Call us at +919081915912 or email info@conveline.com today for detailed information and expert guidance on implementing pallet conveyor systems in your facility.
FAQs
pallet conveyor automated material handling warehouse automation pallet systems industrial conveyors manufacturing efficiency logistics automation pallet transport vertical lifter material handling solutions
Table of Contents
- Introduction